Top 10 Types of High Performance Welding Machines

High performance welding is no longer defined by amperage alone. Modern production demands stable arcs, controlled heat input, repeatable penetration, and dependable uptime. A machine may look powerful on a specification sheet, yet perform poorly beside a drafty workshop door or under fluctuating input voltage. Real performance appears at the weld joint.

John C. Lippold, a respected welding metallurgy expert and professor, has stated, “Welding is a process, not a product.” That reminder shapes this guide. The best equipment supports the entire process, from material preparation to final inspection. It must match the alloy, thickness, joint design, shielding gas, and operator’s working habits. Small details matter. A clean tungsten, dry wire, and steady torch angle can change the bead dramatically.

This overview examines ten major types of high performance welding machines. It considers advanced MIG, TIG, stick, flux-cored, plasma, laser, robotic, multi-process, submerged arc, and resistance systems. Each category offers practical strengths, but none is ideal everywhere. That is easy to overlook.

Some machines excel on thin stainless steel. Others handle heavy structural plate for long production cycles. Important comparisons include duty cycle, waveform control, arc response, cooling design, automation compatibility, maintenance access, and total operating cost. Safety features and documented compliance also deserve close attention.

The ranking is not absolute. Shop conditions vary. A costly machine can still disappoint when its controls are poorly understood. This guide therefore combines technical specifications with field-based judgment, while acknowledging one uncomfortable truth: even excellent equipment cannot repair careless preparation or weak process control.
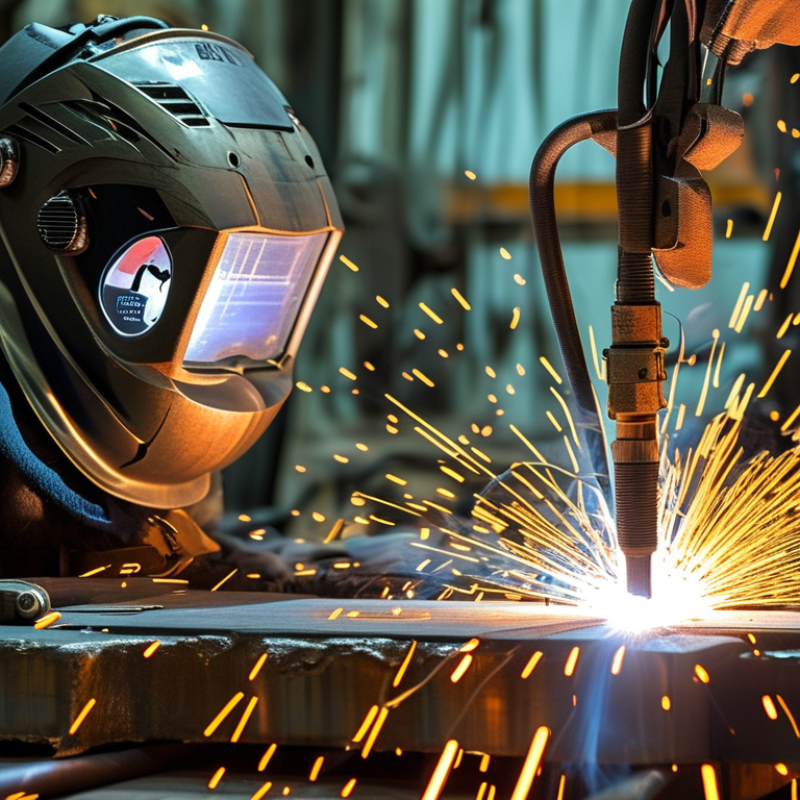
Top 10 Types of High Performance Welding Machines

Definition and Core Features of High-Performance Welding Machines

High-performance welding machines are engineered systems that maintain controlled heat, stable arcs, and consistent results under demanding workloads. They support processes such as MIG, TIG, stick, plasma, and submerged arc welding. Unlike basic equipment, they are designed for accuracy, repeatability, and extended operation. Not merely speed. A high-performance machine must help produce sound welds while reducing rework, distortion, and operator fatigue.

Core features include precise current control, fast arc response, and a high duty cycle. Advanced thermal management protects internal components during long production runs. Digital displays can show amperage, voltage, wire speed, and fault conditions in real time. Some systems store welding parameters, helping technicians repeat qualified settings across different jobs. Strong cable connections and stable wire feeding also matter. Small interruptions can leave visible defects.

From practical workshop experience, performance depends on more than specifications. A clean joint, correct shielding gas, and suitable consumables remain essential. No machine can repair poor preparation. Published duty-cycle figures may also change with ambient temperature, so users should read the full technical data. That matters. Operators sometimes trust automatic settings too quickly, especially on unfamiliar metals. Regular calibration, nozzle inspection, and airflow checks provide more reliable results. Even excellent equipment needs skilled judgment, and that is where real-world performance can become inconsistent.

Ten Major Types and Their Distinct Welding Processes

Top 10 Types of High Performance Welding Machines

High-performance welding machines differ mainly by process, control, and heat delivery. SMAW uses flux-coated electrodes for outdoor structural repairs. GMAW, commonly called MIG, feeds solid wire continuously for fast steel fabrication. FCAW uses flux-cored wire and handles windy, demanding site conditions better. GTAW, or TIG, creates precise arcs for stainless steel, aluminum, and thin sections. SAW buries the arc under granular flux, supporting deep penetration on long, straight joints.

Plasma arc welding concentrates heat through a narrow plasma jet. Resistance spot welding clamps sheets and creates localized heat between electrodes. Resistance seam welding produces overlapping welds for tanks and sealed panels. Laser beam welding delivers a small, intense heat zone and supports automated production. Ultrasonic welding joins certain thin metals through vibration and pressure, without melting the entire joint. The International Energy Agency reported more than 17 million electric cars sold globally in 2024, increasing demand for repeatable battery-pack welding. The International Federation of Robotics recorded 541,302 industrial robot installations in 2023, reinforcing the move toward integrated welding cells.

Data helps, but it is not the whole decision. A machine rated for high output may struggle with poor fit-up, contaminated surfaces, or unstable power. That matters. In practical trials, operators should compare arc stability, spatter, penetration, duty cycle, and repair time. My assessment is imperfect: material thickness, joint access, operator skill, and ventilation can change the ranking completely.

Top 10 Types of High Performance Welding Machines - Ten Major Types and Their Distinct Welding Processes

Rank Machine Type Welding Process Primary Heat Source Electrode or Filler Typical Current / Power Range Suitable Materials Key Performance Advantage Productivity Profile Common Industrial Applications Main Limitation
1 Submerged Arc Welding Machine SAW: continuous wire arc welding beneath granular flux Electric arc between a continuously fed wire and the workpiece Continuous bare wire with granular flux Approximately 300–1,200 A; normally powered by a constant-voltage or constant-current source Carbon steel, low-alloy steel, stainless steel, and selected nickel alloys Very high deposition rate Excellent for long, straight, flat or horizontal welds; often mechanized or automated Pressure vessels, structural beams, storage tanks, large-diameter pipe, shipbuilding, and heavy fabrication Limited visibility and position capability; generally unsuitable for short or highly complex welds
2 Gas Metal Arc Welding Machine GMAW: continuous wire arc welding with external shielding gas Electric arc between a continuously fed consumable wire and the workpiece Solid or metal-cored wire; shielding gas may be argon, carbon dioxide, or a mixture Approximately 50–500 A, depending on wire diameter, material, and transfer mode Carbon steel, stainless steel, aluminum, and many nonferrous alloys High deposition with continuous operation High duty cycle and low electrode waste; well suited to robotic and production welding Automotive structures, transportation equipment, machinery, frames, and general metal fabrication Shielding gas can be disturbed by wind; surface cleanliness and parameter control are important
3 Flux-Cored Arc Welding Machine FCAW: tubular flux-cored wire arc welding Electric arc between a continuously fed tubular wire and the workpiece Self-shielded or gas-shielded flux-cored wire Approximately 100–700 A, depending on wire type and weld position Carbon steel, low-alloy steel, stainless steel, and some wear-resistant alloys High deposition and strong outdoor capability Fast welding with good tolerance for thicker sections; self-shielded variants reduce dependence on bottled gas Heavy equipment, bridges, ship repair, construction steelwork, pipelines, and field fabrication Produces slag that must be removed; smoke and spatter can be higher than with some other processes
4 Tungsten Inert Gas Welding Machine GTAW / TIG: nonconsumable tungsten arc welding Electric arc between a tungsten electrode and the workpiece Nonconsumable tungsten electrode; separate filler rod may be added Approximately 5–500 A; AC is commonly used for aluminum, while DC is common for steels Stainless steel, aluminum, magnesium, titanium, nickel alloys, and thin metals Outstanding weld quality and control Lower deposition rate, but highly precise and suitable for critical root passes and thin materials Aerospace components, food and pharmaceutical equipment, pipework, heat exchangers, and precision fabrication Slower than wire-fed processes; requires high operator skill and clean joint surfaces
5 Plasma Arc Welding Machine PAW: constricted plasma arc welding High-temperature plasma arc formed through a fine copper nozzle Nonconsumable tungsten electrode; filler wire may be used Approximately 5–300 A for common production applications Stainless steel, nickel alloys, titanium, carbon steel, and other electrically conductive metals Deep, narrow penetration Can operate in micro-plasma mode for thin sheet or keyhole mode for deeper fusion Precision tubing, aerospace parts, instrumentation, electronics enclosures, and automated fabrication Higher equipment complexity; nozzle alignment and maintenance affect arc stability
6 Laser Beam Welding Machine LBW: focused laser beam fusion welding Concentrated optical energy from a laser source Usually autogenous; wire filler can be added when required Common industrial systems range from approximately 1–20 kW of laser power Steels, stainless steel, aluminum, titanium, nickel alloys, and selected dissimilar-metal combinations Very low heat input and high precision Extremely fast travel speeds, narrow heat-affected zones, and strong suitability for robotic production Automotive batteries, electronics, medical devices, precision assemblies, and aerospace components High initial cost; joint fit-up, reflectivity, safety controls, and process monitoring are critical
7 Electron Beam Welding Machine EBW: focused electron beam fusion welding in vacuum or controlled atmosphere Kinetic energy of accelerated electrons converted into heat at the joint Usually autogenous; filler wire is used for selected applications Typically approximately 30–150 kV accelerating voltage, with beam power selected for joint depth Steels, titanium, nickel alloys, refractory metals, and some dissimilar-metal joints Exceptional penetration-to-width ratio Deep, narrow welds with low distortion and strong repeatability in controlled production Aerospace engine parts, transmission components, high-integrity pressure parts, and specialized scientific equipment Vacuum chamber size can limit workpiece dimensions; equipment and safety requirements are substantial
8 Resistance Spot Welding Machine RSW: localized resistance heating between clamped electrodes Joule heat generated by electrical resistance at the faying surfaces No separate filler or consumable electrode; copper-alloy electrodes provide current and pressure Approximately 5–100 kA welding current, generally delivered in short timed pulses Low-carbon steel, galvanized steel, stainless steel, and selected aluminum sheet Very fast repeatable joints Excellent for high-volume automation; individual welds can be completed in fractions of a second Vehicle bodies, appliances, cabinets, metal furniture, and sheet-metal assemblies Primarily suited to overlapping sheet; access is needed from both sides and electrode wear must be controlled
9 Friction Stir Welding Machine FSW: solid-state joining with a rotating, nonconsumable tool Frictional and plastic-deformation heat generated by the rotating tool Nonconsumable tool; no filler metal is normally required Machine force and spindle torque are application-dependent; typical tool speeds are approximately 200–3,000 rpm Aluminum alloys, magnesium alloys, copper alloys, titanium, and selected dissimilar materials Low distortion and strong solid-state joints Highly repeatable and well suited to long linear welds and automated production Rail vehicles, aircraft structures, ship panels, battery trays, heat sinks, and aluminum extrusions Requires rigid fixturing and specialized tooling; start and finish conditions need careful planning
10 Electroslag Welding Machine ESW: vertical welding through electrically conductive molten slag Electrical resistance heat generated in molten slag Continuously fed wire or electrode; water-cooled shoes contain the molten pool Often approximately 600–1,500 A for heavy-section production work Thick carbon steel and low-alloy steel sections Single-pass capability for very thick joints High productivity on vertical joints with large thicknesses; minimizes the need for repeated passes Heavy structural columns, large castings, ship sections, pressure equipment, and thick plate fabrication Restricted to suitable vertical joints; high heat input can affect toughness and microstructure

Power Sources, Materials, and Operating Capabilities

High-performance welding machines differ mainly in their power sources, material control, and operating range.

Ten useful categories include transformer welders, inverter welders, engine-driven units, pulse MIG machines, TIG systems, multi-process welders, submerged arc machines, resistance welders, plasma systems, and laser welders.

Transformer models provide stable output for heavy steel work. Inverter designs are lighter and offer finer arc control. Engine-driven units support field repairs where electricity is unavailable. Pulse MIG reduces heat input and helps weld aluminum with less distortion.

Material selection changes the machine decision.
Steel often needs strong penetration and a high duty cycle. Stainless steel benefits from controlled heat and clean shielding gas. Aluminum requires adjustable waveform control because it conducts heat quickly. Titanium and nickel alloys demand precise current control, stable gas coverage, and careful surface preparation.

Operating capabilities also matter.

Check amperage range, duty cycle, wire speed, arc-start quality, remote control, and automation compatibility.

A powerful machine is not automatically the correct machine.

I once valued maximum amperage too highly; actual joint thickness and production rhythm mattered more.

Tips:

Test the machine on scrap with the same material and thickness. Watch the arc, bead profile, and heat tint. Keep a record of voltage, current, travel speed, and gas flow. Small adjustments often prevent porosity and undercut. Leave room for human judgment. Settings can be technically correct yet unsuitable for a particular joint, position, or operator.

Performance Comparison by Precision, Speed, and Application

High-performance welding machines differ sharply in precision, speed, and application. The leading ten types include inverter MIG, pulse MIG, AC/DC TIG, plasma arc, laser, resistance spot, seam, submerged arc, robotic multi-process, and hybrid welding systems. AC/DC TIG offers the finest control for thin stainless steel and aluminium, while pulse MIG deposits metal faster with lower heat input. Laser welding creates narrow, clean seams, but it demands accurate joint preparation and stable fixturing. Precision has a price.

For production speed, submerged arc welding remains effective on long, thick carbon-steel joints. Resistance spot and seam systems suit repeatable sheet-metal work, where cycle time matters more than visual flexibility. Robotic multi-process cells improve consistency during extended runs. The International Federation of Robotics’ World Robotics 2024 report recorded 541,302 industrial robot installations worldwide in 2023, showing stronger demand for automated production. However, robot numbers do not guarantee better welds. Poor programming still produces expensive defects.

Application should guide selection, not impressive specifications. Plasma systems handle controlled cutting and welding, while compact inverter machines support field repairs and variable power supplies. AWS workforce data projects a need for about 330,000 new welding professionals by 2026, increasing pressure for easier controls and repeatable results. My practical concern is calibration: even a precise laser system can fail when operators overlook fit-up, shielding gas flow, or surface contamination. These details are easy to underestimate. Precision may be wasted without disciplined inspection.

Selection Criteria, Safety Requirements, and Maintenance Considerations

High-performance welding machines include inverter MIG/MAG, AC/DC TIG, pulse, multiprocess, resistance spot, submerged arc, plasma, laser, robotic, and automated systems. Selection should begin with the joint, material, thickness, and production rhythm. Check rated output, duty cycle, input voltage, arc stability, waveform control, portability, and service access. A machine rated at 300 amps may overheat quickly at continuous production loads. Duty cycle matters.

Safety cannot depend on the operator’s memory. The WHO/ILO Joint Estimates, published in 2021, linked 1.9 million deaths in 2016 to work-related risk factors. Welding areas need local exhaust ventilation, suitable eye protection, flame-resistant clothing, electrical grounding, and controlled gas storage. IARC classifies welding fumes as carcinogenic to humans. Fume extraction must match the process, not merely the room size. Fit matters. A clean-looking booth may still contain hazardous particles.

Maintenance records should track torch condition, cable insulation, earth-clamp resistance, cooling flow, gas leaks, and output calibration. ISO 17662 supports calibration and verification for welding equipment. Inspect consumable contact parts before arc instability damages the workpiece. Keep it practical. Operators should compare actual amperage with the machine display, because digital readings can drift. A useful improvement is a short pre-shift checklist, although rushed teams may skip it. Supervisors should review those skipped items instead of treating paperwork as proof of safety.

Translate