2026 Best Manufacturing Process Efficiency Solutions

Manufacturing process efficiency is becoming a boardroom priority, not merely a factory-floor ambition. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturing leaders expect smart manufacturing to become a major competitiveness driver within five years. The same study reported that 83% believe it will transform production. These figures reveal strong confidence, but they do not guarantee successful implementation.

Taiichi Ohno, the architect of the Toyota Production System, observed, “All we are doing is looking at the time line from order to cash, and reducing it.” His principle still applies beside modern sensors, robotics, and artificial intelligence. Efficient plants measure the details: changeover minutes, first-pass yield, unplanned downtime, energy use, and operator walking distance. A dashboard is not improvement. It only exposes the problem.

The World Economic Forum’s Global Lighthouse Network has documented factories achieving substantial gains in productivity, quality, and sustainability through connected technologies and disciplined operating models. However, these examples are not universal templates. Smaller plants may lack clean data, skilled analysts, or capital for rapid automation. Even advanced facilities still experience bottlenecks, false alarms, and inconsistent work standards. That is the uncomfortable part.

The 2026 Best Manufacturing Process Efficiency Solutions should therefore be judged by measurable outcomes, not impressive demonstrations. Strong solutions connect people, machines, and decisions. They reduce waste without weakening safety or product quality. They also support continuous learning when reality disrupts the plan. Efficiency is never finished.
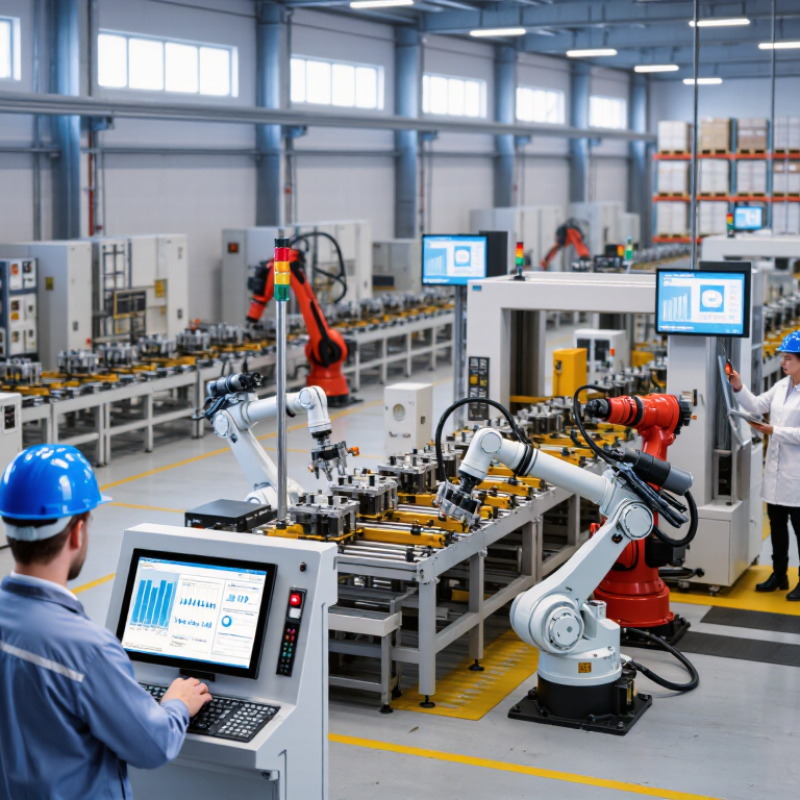
2026 Best Manufacturing Process Efficiency Solutions

Manufacturing Process Efficiency: Definition, Scope, and Core Principles

Manufacturing process efficiency means producing consistent output with fewer wasted materials, minutes, movements, and energy units. Its scope reaches beyond machine speed. It includes product design, scheduling, equipment reliability, workforce skills, quality control, logistics, and maintenance. A faster line is not efficient if it creates more defects.

Deloitte’s 2024 Smart Manufacturing and Operations Survey reports that 92% of surveyed manufacturers view smart manufacturing as a main competitiveness driver within three years. The figure signals urgency, not automatic success. Core principles include measuring process variation, standardizing repeatable work, and solving root causes before adding technology. The International Energy Agency reports that industry accounts for roughly 37% of global final energy use. Energy efficiency therefore belongs inside operational planning, not in a separate sustainability file. Small leaks matter.

Useful solutions connect real-time production data with practical decisions. Operators should see downtime minutes, first-pass yield, changeover time, and energy per unit near the workstation. The World Economic Forum’s Global Lighthouse Network has documented productivity gains of up to 50% in selected advanced manufacturing transformations, but these results are not universal. Local constraints matter. A sensor may detect vibration, yet a delayed spare part can still stop production. Human experience remains essential. Process teams should test improvements in controlled steps, record exceptions, and challenge clean-looking dashboards. Efficiency is measurable, but never perfectly tidy.

2026 Best Manufacturing Process Efficiency Solutions

Manufacturing Process Efficiency: Definition, Scope, and Core Principles

Overall Equipment Effectiveness (OEE) combines availability, performance, and quality: OEE = Availability × Performance × Quality. The commonly cited world-class reference levels are approximately 90% availability, 95% performance, and 99.9% quality, producing an OEE of about 85%. These indicators help manufacturers identify downtime, speed losses, and defect-related waste.

Reference basis: widely used OEE benchmark thresholds in manufacturing operations; no company-specific data is included.

Key Technologies for Improving Manufacturing Process Efficiency

2026 Best Manufacturing Process Efficiency Solutions

Key Technologies for Improving Manufacturing Process Efficiency

Manufacturers are improving efficiency by connecting machines, people, and production data. Industrial sensors can track temperature, vibration, pressure, and cycle time in real time. A small vibration change may reveal bearing wear before a line stops. This supports planned maintenance instead of costly emergency repairs.

Manufacturing execution systems can link work orders with equipment status and quality records. Operators gain a clearer view of bottlenecks, rework, and material delays. Edge computing processes urgent signals near the machine, reducing dependence on distant servers. Cloud platforms then support wider analysis across plants. Digital twins can test layout changes or production schedules before physical adjustments are made.

Artificial intelligence also supports predictive maintenance and visual inspection. Cameras can identify surface defects at consistent speeds, while algorithms detect unusual process patterns. However, poor data creates poor decisions. Sensors need calibration, and historical records may contain gaps. The first prediction is rarely perfect. Engineers should compare system alerts with physical inspections and operator experience. Human judgment still matters, especially when a process changes unexpectedly. Energy monitoring adds another practical layer by showing where compressed air, heat, or electricity is being wasted. Small leaks can remain invisible for months. Measuring them makes improvement easier to verify.

Step-by-Step Methods for Assessing Production Performance

2026 Best Manufacturing Process Efficiency Solutions

Step-by-Step Methods for Assessing Production Performance

A reliable performance assessment begins on the factory floor, not in a spreadsheet. Walk through each process and record cycle time, changeover duration, downtime, and output. Compare actual cycle time with takt time, which reflects customer demand. Measure first-pass yield and scrap at every workstation. These details reveal hidden losses that monthly totals often miss.

Next, verify the data with operators and maintenance staff. Their experience can explain repeated stops, material delays, or difficult adjustments. Calculate Overall Equipment Effectiveness using availability, performance, and quality. Then identify the constraint limiting total production. Do not improve every station at once. Focus on the bottleneck and test one controlled change. Early results may look impressive but still mislead. I have seen incomplete downtime codes produce confident, inaccurate conclusions.

Tips: Use consistent time periods. Separate planned and unplanned stops. Photograph recurring defects. Review results weekly. Keep the method simple enough for every shift to follow. A short observation can expose more than a complex report. Recheck measurements after changes, because efficiency gains sometimes move problems downstream. Workers may resist a new metric, and that response deserves investigation rather than blame.

Implementation Strategies for Manufacturing Efficiency Solutions

Implementation Strategies for Manufacturing Efficiency Solutions

Manufacturing efficiency improves when implementation begins with evidence, not assumptions. Walk the production floor and record changeover time, idle minutes, rework, energy use, and safety observations. Speak with machine operators. Their practical experience often reveals delays hidden in monthly reports.

Start small. Select one line with repeated stoppages and establish a four-week baseline. Define measurable targets, such as reducing changeover time by 15% or cutting rework by 10%. Configure digital monitoring around those targets, rather than collecting data without purpose. Train supervisors and operators together, using real production scenarios and simple visual instructions. That builds trust.

Our pilot was not perfect. Early sensor readings conflicted with manual logs, and one dashboard encouraged teams to chase speed over quality. We corrected the data rules and added quality checks before expanding. Review results during short weekly meetings, then document each adjustment. Keep maintenance, engineering, production, and quality staff involved. A solution that works technically may still fail operationally. Plan for staff feedback, equipment variation, cybersecurity controls, and scheduled maintenance from the beginning. Continuous improvement needs discipline, but it also needs room to question the original plan.

2026 Best Manufacturing Process Efficiency Solutions — Implementation Strategies for Manufacturing Efficiency Solutions
Efficiency Solution Primary Process Problem Key Performance Dimension Typical Improvement Target Implementation Horizon Investment Level Recommended Implementation Strategy Critical Success Indicator
Lean Value-Stream Improvement Excess waiting, transport, inventory, overprocessing, and production bottlenecks Lead time and work-in-process inventory Lead time reduction of 15–30%; work-in-process reduction of 10–25% 3–9 months Medium Map the current-state value stream, identify the constraint, redesign the future state, and run weekly improvement events using measured before-and-after results. Shorter order-to-ship cycle with no deterioration in delivery reliability or product quality
Overall Equipment Effectiveness Management Unplanned downtime, slow cycles, and production losses that are not consistently categorized Availability, performance, and quality OEE improvement of 5–15 percentage points when reliable loss data and corrective actions are established 2–6 months Low to Medium Define standard loss codes, validate downtime records, establish daily tier meetings, and prioritize the three largest recurring losses. Validated loss data and sustained reduction in the largest sources of equipment loss
Total Productive Maintenance Recurring equipment failures, delayed maintenance, and poor operator ownership Mean time between failures and planned maintenance compliance Unplanned downtime reduction of 10–25%; planned-maintenance compliance above 90% 6–12 months Medium Start with critical assets, create autonomous-maintenance checklists, improve preventive-maintenance intervals, and review failure causes monthly. Fewer repeat failures and a rising percentage of planned maintenance work
Quick Changeover and SMED Long setup times that restrict batch-size flexibility and increase idle capacity Setup and changeover duration Setup-time reduction of 30–50% after separating internal and external activities 1–4 months per selected process Low to Medium Record the changeover, separate activities that require a stopped machine, standardize tools and settings, and use visual setup instructions. Reduced changeover time with stable first-piece quality after each setup
Statistical Process Control Process variation, unstable output, and late detection of defects Process capability and defect rate Defect reduction of 10–30% in targeted characteristics; improved process-capability stability 2–6 months Low Select critical-to-quality characteristics, verify measurement-system reliability, establish control limits, and train operators to react to special causes. Fewer special-cause events and lower first-pass yield losses
Digital Production Monitoring Delayed production information and manual data collection errors Data availability and response time Loss-reporting delay reduced from hours or shifts to near real time; improved schedule adherence 3–9 months Medium to High Begin with one line, connect only the required data sources, define common metric rules, and use dashboards for daily operational decisions rather than passive reporting. Operators and supervisors act on accurate production data during the same shift
Predictive Maintenance Analytics Unexpected failures on high-value or high-criticality assets Failure prediction and maintenance effectiveness Unplanned downtime reduction of 10–20% on suitable assets after sufficient historical data is available 6–18 months High Rank assets by criticality, verify sensor and maintenance-history quality, pilot on failure-prone equipment, and connect alerts to defined work-order actions. Actionable alerts that prevent failures without creating excessive false alarms
Standardized Digital Work Instructions Operator-to-operator variation, training gaps, and inconsistent work methods Training time, cycle consistency, and first-pass yield Training time reduction of 20–40%; measurable reduction in method-related defects 1–3 months per process family Low to Medium Document the best-known method, use concise visual steps, include quality checkpoints, obtain operator review, and control revisions at the point of use. High instruction adherence and consistent results across shifts and experience levels
Quality-at-the-Source Defects passed between operations and costly end-of-line rework First-pass yield and internal defect cost Internal rework reduction of 15–30% in targeted processes 2–6 months Low to Medium Move inspection and error-proofing to the point of work, define stop-and-call criteria, and review defect causes within one production cycle. Defects are detected and contained at the originating operation
Energy and Utility Optimization Unmeasured consumption, idle operation, leaks, and inefficient equipment settings Energy intensity per unit of output Energy-use reduction of 5–15% through measurement, operating controls, and targeted maintenance 3–12 months Medium Establish a baseline by production area, identify significant energy users, correct leaks and idle running, and track consumption against production volume. Lower energy intensity without reducing throughput, safety, or product conformity
Material Flow and Line Balancing Uneven workloads, queue formation, excess movement, and constrained workstations Throughput, takt adherence, and labor utilization Throughput improvement of 5–15%; non-value-added movement reduction of 10–25% 2–5 months Medium Calculate takt demand, measure task times, rebalance work content, shorten travel paths, and use supermarkets or point-of-use replenishment where appropriate. More even station loading and improved flow with no increase in safety risk
Closed-Loop Continuous Improvement Improvement projects that stop after implementation or lack verified financial impact Verified savings and action closure rate Action-closure rate above 85%; sustained benefits verified over at least three operating months Ongoing; first results within 1–3 months Low Use a standard problem-solving method, assign accountable owners, confirm root causes, verify benefits with finance and operations, and audit improvements after implementation. Benefits remain visible after the project team withdraws
Planning ranges are typical operational targets for properly scoped improvement programs, not guaranteed results. Baselines should be established using consistent definitions, verified measurement systems, product mix, operating hours, and safety and quality requirements before targets are approved.

Measurement, Optimization, and Future Trends in 2026

2026 Best Manufacturing Process Efficiency Solutions

Measurement now defines manufacturing efficiency. The 2024 Global Smart Manufacturing Survey reported that 86% of manufacturing leaders consider smart operations essential for competitiveness. Yet many factories still measure output without measuring hidden losses. A stopped conveyor, repeated inspection, or five-minute changeover can quietly reshape the daily cost curve. Effective 2026 programs connect machine data, energy use, quality results, and labor time in one operating view. The data must be trustworthy. Bad sensor calibration creates precise-looking mistakes.

Optimization should begin with the constraint, not the newest technology. Real production experience shows that reducing changeover time may deliver more value than adding another dashboard. The World Economic Forum’s Global Lighthouse Network has documented double-digit improvements in productivity, lead time, and energy performance across advanced sites. However, those results are not automatic. Local skills, maintenance discipline, and process ownership often decide whether improvements survive beyond a pilot. This is where many projects weaken.

Future efficiency will depend on adaptive systems, industrial artificial intelligence, and lower-carbon production planning. The International Energy Agency continues to identify industry as a major source of global energy demand, making energy measurement a business priority. Operators may soon receive live recommendations for scheduling, maintenance, and material flow. That sounds efficient. It can also overwhelm workers. Human review, clear exception rules, and regular model testing remain necessary, especially when demand changes or data becomes incomplete.

Translate