Modern metal forming is the controlled reshaping of metal through force, heat, and carefully designed tooling. It supports vehicle panels, aircraft brackets, medical instruments, appliances, and structural components. The process may involve stamping, forging, rolling, extrusion, bending, or deep drawing. Each method changes the material without removing large amounts of it.
Professor Taylan Altan, a leading authority in metal forming, describes it clearly: “Metal forming is the process of changing the shape of a metal part by plastic deformation.” This definition explains the central idea. A press pushes a steel blank into a die, while the material flows and keeps its new shape. Engineers monitor force, friction, temperature, thickness, and springback. Small changes can create wrinkles, cracks, or dimensional errors.
Modern metal forming is not simply about applying greater pressure. It is about controlling material behavior. Computer simulations can predict deformation before production begins. Sensors can then verify force and position during each cycle. Still, prediction is never perfect. Material batches vary, tools wear, and real surfaces behave differently from laboratory samples. That uncertainty deserves attention.
A reliable forming strategy combines engineering calculations, production experience, testing, and quality inspection. This article explains how the process works, why different metals respond differently, and where modern technologies improve accuracy. The goal is practical understanding, not an idealized picture. Real factories are more complicated. That is where expertise matters.
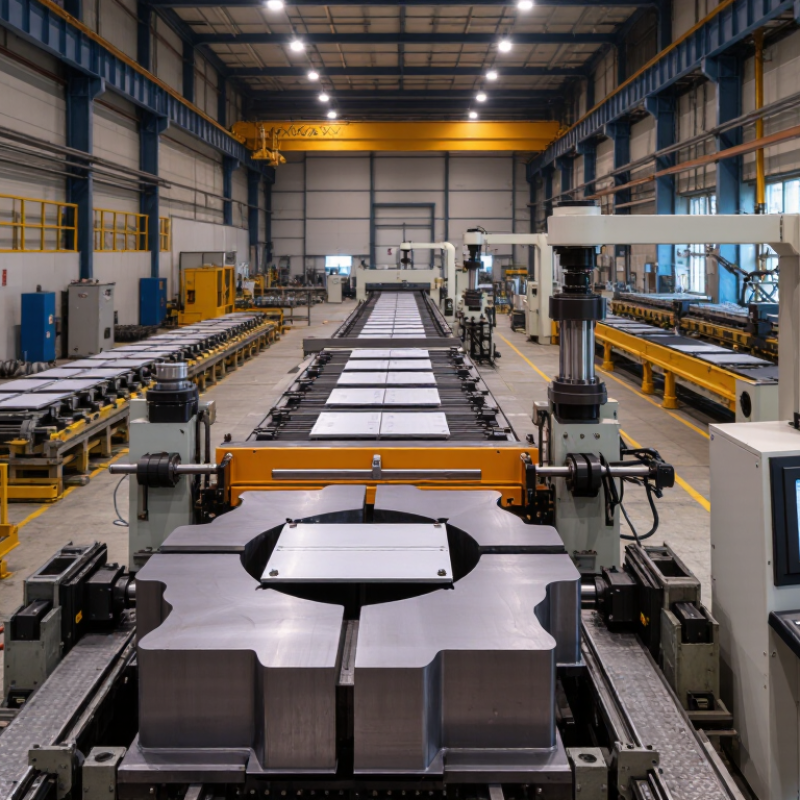
Modern metal forming reshapes solid metal through controlled force, heat, and movement. Unlike cutting, it preserves most material rather than removing it. Common methods include rolling, forging, stamping, extrusion, bending, and deep drawing. The goal is not simply a new shape. It is a reliable part with predictable strength, dimensions, and surface condition. In practical work, engineers select a process according to alloy behavior, thickness, geometry, and production volume.
The goal is not simply a new shape. It is a reliable part with predictable strength, dimensions, and surface condition.
The core principle is plastic deformation. Pressure must exceed the metal’s yield strength, but remain controlled enough to prevent cracking or excessive thinning. Temperature changes this balance. Warm or hot forming can improve ductility, while cold forming often increases strength through work hardening. Friction, tool radius, lubrication, and forming speed also affect material flow. A small radius may create a visible split along an otherwise accurate edge. This is where theory meets the press. Not always elegant.
Modern systems combine forming analysis, sensors, and dimensional inspection.
Operators watch force curves, die alignment, springback, and surface marks. Engineers may adjust blank-holder pressure or compensate tool geometry after trial parts. First setups often fail. That is not failure, but it deserves investigation. A useful process links material data with shop-floor evidence, then records each correction. Even so, simulations can miss local defects, especially when material variation or lubrication changes during production.
Watch the edges.
What Is Modern Metal Forming and How Does It Work?
Modern metal forming changes a workpiece without removing large amounts of material. The process uses controlled force, heat, or both. Steel offers strength, while aluminum reduces weight. Copper supports electrical applications, and titanium handles demanding conditions. Each material behaves differently under pressure. Its thickness, grain structure, and temperature affect the final shape. In practical workshops, material certificates and sample tests help confirm reliable performance.
The main tools include dies, punches, rollers, mandrels, clamps, and forming blocks. A die guides the metal, while a punch applies direct force. Roll forming uses several stations to shape sheet gradually. Deep drawing stretches flat sheet into cups or housings. Forging presses compress heated billets between shaped tools. Lubrication reduces friction and limits surface damage. Small scratches can become serious defects later.
Equipment selection depends on shape, volume, and tolerances. Mechanical presses suit fast, repeatable production. Hydraulic presses provide adjustable force and longer forming strokes. Servo-driven systems can control movement more precisely. Sensors monitor pressure, position, and temperature during production. Coordinate measuring equipment checks dimensions after forming. I have found that inspection during setup prevents expensive rework. A perfect setup rarely exists. Tool wear, springback, and uneven lubrication still create surprises. Engineers must adjust forming speed, clearance, or heat carefully. That judgment often matters as much as the machine itself.
| Forming Process | How It Works | Common Materials | Primary Tools | Main Equipment | Typical Products | Key Advantages | Important Controls |
|---|---|---|---|---|---|---|---|
| Rolling | A slab, billet, or strip passes between rotating rolls that reduce thickness or change the cross-sectional profile. | Carbon steel, stainless steel, aluminum alloys, copper alloys, titanium alloys, and nickel alloys. | Flat rolls, shaped rolls, guide plates, edging tools, and roll-gap adjustment systems. | Two-high, four-high, or multi-roll mills; hot-strip mills; cold-reduction mills; and leveling lines. | Sheet, plate, strip, bars, rails, structural sections, and foil. | High throughput, consistent thickness, and efficient production of long products. | Roll gap, reduction per pass, rolling speed, temperature, lubrication, and strip tension. |
| Forging | Compressive forces from hammers or presses plastically deform a billet into the required shape, usually above or below the recrystallization temperature. | Carbon and alloy steels, stainless steels, aluminum alloys, titanium alloys, and nickel-based alloys. | Open dies, impression dies, punches, mandrels, swages, and trimming dies. | Mechanical or hydraulic presses, drop hammers, induction heaters, furnaces, and die-handling systems. | Gears, shafts, connecting rods, fasteners, turbine parts, and high-strength structural components. | Improved grain flow, high strength, good fatigue resistance, and reduced internal porosity. | Billet temperature, die temperature, deformation rate, lubrication, draft, and final cooling rate. |
| Extrusion | A billet is pushed through a die opening, producing a continuous profile with the die's cross-sectional shape. | Aluminum alloys, copper alloys, brass, magnesium alloys, lead, and selected steels. | Solid dies, hollow dies, mandrels, containers, dummy blocks, and pullers. | Hydraulic extrusion presses, billet heaters, die ovens, runout tables, stretchers, and cut-off saws. | Window frames, heat sinks, tubes, channels, rails, rods, and custom structural profiles. | Complex constant profiles, good material utilization, and strong directional properties. | Extrusion ratio, billet temperature, ram speed, die design, friction, and exit cooling. |
| Deep Drawing | A flat sheet blank is pulled through a die by a punch to form a cup or hollow component without intentionally cutting the material. | Low-carbon steel, stainless steel, aluminum alloys, copper, brass, and selected nickel alloys. | Punches, drawing dies, blank holders, beads, ironing rings, and forming inserts. | Single-action or double-action presses, transfer presses, lubrication systems, and automated blank feeders. | Cans, sinks, housings, fuel containers, covers, and automotive body parts. | Seamless hollow shapes, repeatable dimensions, and efficient high-volume production. | Blank-holder force, punch radius, die radius, lubrication, drawing ratio, and sheet anisotropy. |
| Stamping and Bending | A press and die set cut, bend, emboss, or form sheet metal through one or more controlled strokes. | Mild steel, high-strength steel, stainless steel, aluminum alloys, brass, and copper. | Punches, dies, V-dies, wiping dies, embossing tools, blanking tools, and progressive dies. | Mechanical presses, servo presses, press brakes, coil feeders, straighteners, and transfer systems. | Brackets, clips, panels, electrical enclosures, appliance parts, and vehicle components. | Fast cycle times, repeatability, automation potential, and low unit cost at production volume. | Bend allowance, springback, punch-die clearance, press force, tool alignment, and feed accuracy. |
| Wire and Tube Drawing | Wire or tube is pulled through a die to reduce its diameter, improve surface finish, or control dimensional accuracy. | Carbon steel, stainless steel, copper, aluminum, titanium, and nickel alloys. | Drawing dies, mandrels, plugs, capstans, pointed ends, and sizing tools. | Bull-block or multi-die drawing machines, payoff reels, take-up reels, annealing furnaces, and lubrication units. | Electrical wire, cables, precision tubes, springs, medical tubing, and fine rods. | Excellent dimensional control, smooth surfaces, and increased strength through cold work. | Die angle, reduction per pass, drawing speed, lubrication, back tension, and intermediate annealing. |
| Roll Forming | A continuous strip moves through successive roll stations, with each station gradually bending it into a finished profile. | Galvanized steel, carbon steel, stainless steel, aluminum, and coated sheet materials. | Contour rolls, forming stands, side rolls, guides, cutoff dies, and punching units. | Continuous roll-forming lines, decoilers, straighteners, in-line punches, welders, and flying saws. | Roofing sections, framing studs, rails, channels, door tracks, and cable trays. | High production speed, long continuous lengths, low scrap, and consistent profile geometry. | Roll alignment, flower pattern, strip tension, pass-line height, edge control, and springback compensation. |
| Hydroforming | Fluid pressure forces sheet or tube material against a die, creating complex shapes with relatively uniform wall distribution. | Low-carbon steel, stainless steel, aluminum alloys, copper alloys, and high-strength steels. | Hydroforming dies, seals, axial punches, tube end-feeders, and pressure intensifiers. | High-pressure fluid systems, hydraulic presses, pressure-control units, forming dies, and digital monitoring systems. | Tubular frames, exhaust components, manifolds, lightweight structural parts, and complex panels. | Fewer joints, reduced part count, good dimensional accuracy, and efficient lightweight design. | Fluid pressure, axial feed, sealing force, material hardening, friction, and pressure-time profile. |
Modern metal forming turns flat sheets, bars, or billets into precise components through controlled force. The sequence begins with material selection. Engineers check grade, thickness, grain direction, and ductility. World Steel Association data reports 1.89 billion tonnes of crude steel production in 2023. That scale makes process control essential, not optional.
The workpiece is then cut and cleaned. Lubricant reduces friction between the material and tooling. In stamping, a punch drives sheet metal into a die. Forging compresses heated or cold metal between shaped tools. Rolling reduces thickness through rotating rollers. Operators monitor force, temperature, speed, and tool alignment during every cycle. After forming, technicians inspect dimensions, surface marks, cracks, and springback. A coordinate measuring machine may compare the part with its digital model. The sequence often needs adjustment. Real metal rarely behaves perfectly.
Tips: Keep material certificates with each production batch. Record forming force and temperature, not only final dimensions. Use gradual tool changes when springback appears. The International Energy Agency’s Energy Technology Perspectives 2024 states that industry uses about 37% of global final energy. Better lubrication, shorter heating cycles, and accurate tooling can reduce wasted energy and scrap. However, efficiency should not compromise inspection. A faster press cycle may create hidden fractures. That mistake can survive a quick visual check.
Modern metal forming reshapes solid metal through controlled force, heat, or pressure. Unlike cutting, it preserves most material and redirects its grain flow. Engineers select a process according to alloy strength, part geometry, production volume, and required accuracy. The choice is rarely simple.
Rolling passes heated or cold metal between rotating rolls. It produces sheet, plate, rails, and structural sections with consistent thickness.
Forging compresses billets between dies, improving strength around demanding areas such as shafts, gears, and suspension components.
Extrusion pushes a heated billet through a shaped opening. This method creates long profiles for frames, heat exchangers, and lightweight transport structures.
Stamping uses dies and presses to make panels, brackets, and enclosures at high volume. It is fast, but springback can distort precise shapes.
Deep drawing forms flat sheet into cups, tanks, and protective housings.
Tube drawing reduces diameter while improving dimensional control.
Hydroforming uses fluid pressure to create complex hollow parts with fewer welds.
Incremental sheet forming suits prototypes and low-volume components because flexible tooling reduces setup costs.
Superplastic forming can produce intricate, lightweight parts from specialized alloys, although it needs slow cycles and strict temperature control.
Additive metal forming is also developing, yet surface finish and repeatability still require careful inspection.
No method is universally best. Real production often reveals small cracks, uneven thickness, or unexpected springback. Engineers use simulation, test coupons, dimensional checks, and process adjustments to manage these problems. A design that appears efficient on paper may still waste time during trimming, heat treatment, or quality verification.
Modern metal forming shapes sheet or solid metal through stamping, forging, rolling, bending, and hydroforming. Computer-controlled presses improve repeatability, while sensors track force, temperature, speed, and tool position. In production, quality control begins before the press starts. Engineers verify material certificates, die alignment, lubrication, and first-piece dimensions.
The 2024 World Robotics report recorded 541,302 industrial robot installations worldwide in 2023. That growth supports automated loading, vision inspection, and measurement near the forming line. However, automation does not guarantee quality. A camera may detect a surface crack but miss internal stress or springback. Operators still need calibrated gauges, sampling plans, and process capability studies. A clean dashboard can hide a poor measurement system.
Modern forming reduces machining waste and can produce lightweight parts with consistent strength. High-strength steel and aluminum alloys also support lower vehicle weight. Yet these materials demand greater forming force and tighter tool control. The World Steel Association reported approximately 1.89 billion tonnes of crude steel production in 2023, showing the scale of metal processing behind industrial supply chains. Energy use, die wear, noise, and expensive tooling remain practical limitations. Large presses also require substantial floor space and safety controls. No inspection plan is perfect. In my view, manufacturers sometimes overtrust software and underinvest in operator judgment. The better approach combines real-time data, physical inspection, documented corrective actions, and experienced review. Data source: International Federation of Robotics, World Robotics 2024; World Steel Association, World Steel in Figures 2024.